How to Evaluate the Quality and Condition of Surplus Industrial Products
Surplus industrial products can offer manufacturers, contractors and plant operators an opportunity to acquire equipment, components and materials at significantly lower prices than new products. However, a low purchase price does not necessarily mean a good deal.
Whether the surplus item is a pump, motor, compressor, valve, electrical component, processing machine or spare part, buyers need to establish what they are actually purchasing before committing to a transaction.
A structured inspection can reveal corrosion, wear, missing components, previous repairs, operating damage and other issues that may not be obvious from photographs or a product description. Industry inspection practices also emphasize the importance of documentation, testing and qualified inspection personnel when assessing equipment condition.
Start With the Product's Identity and Specifications
The first step in evaluating a surplus industrial product is confirming exactly what the item is.
Buyers should verify:
Manufacturer and model
Serial number
Manufacturing date
Equipment type
Capacity and operating range
Power requirements
Dimensions and weight
Material of construction
Applicable standards
Original equipment specifications
Available accessories and components
This information should be compared with the seller's description and, where possible, the manufacturer's original documentation.
A mismatch between the advertised specifications and the equipment's nameplate or documentation can indicate that the product is not suitable for the intended application.
For rotating machinery and other complex equipment, buyers should pay particular attention to major components rather than focusing only on external appearance. Used-equipment inspection guidance, for example, recommends examining high-value components such as engines, transmissions, hydraulic pumps and joints early in the inspection process.
Examine the Physical Condition
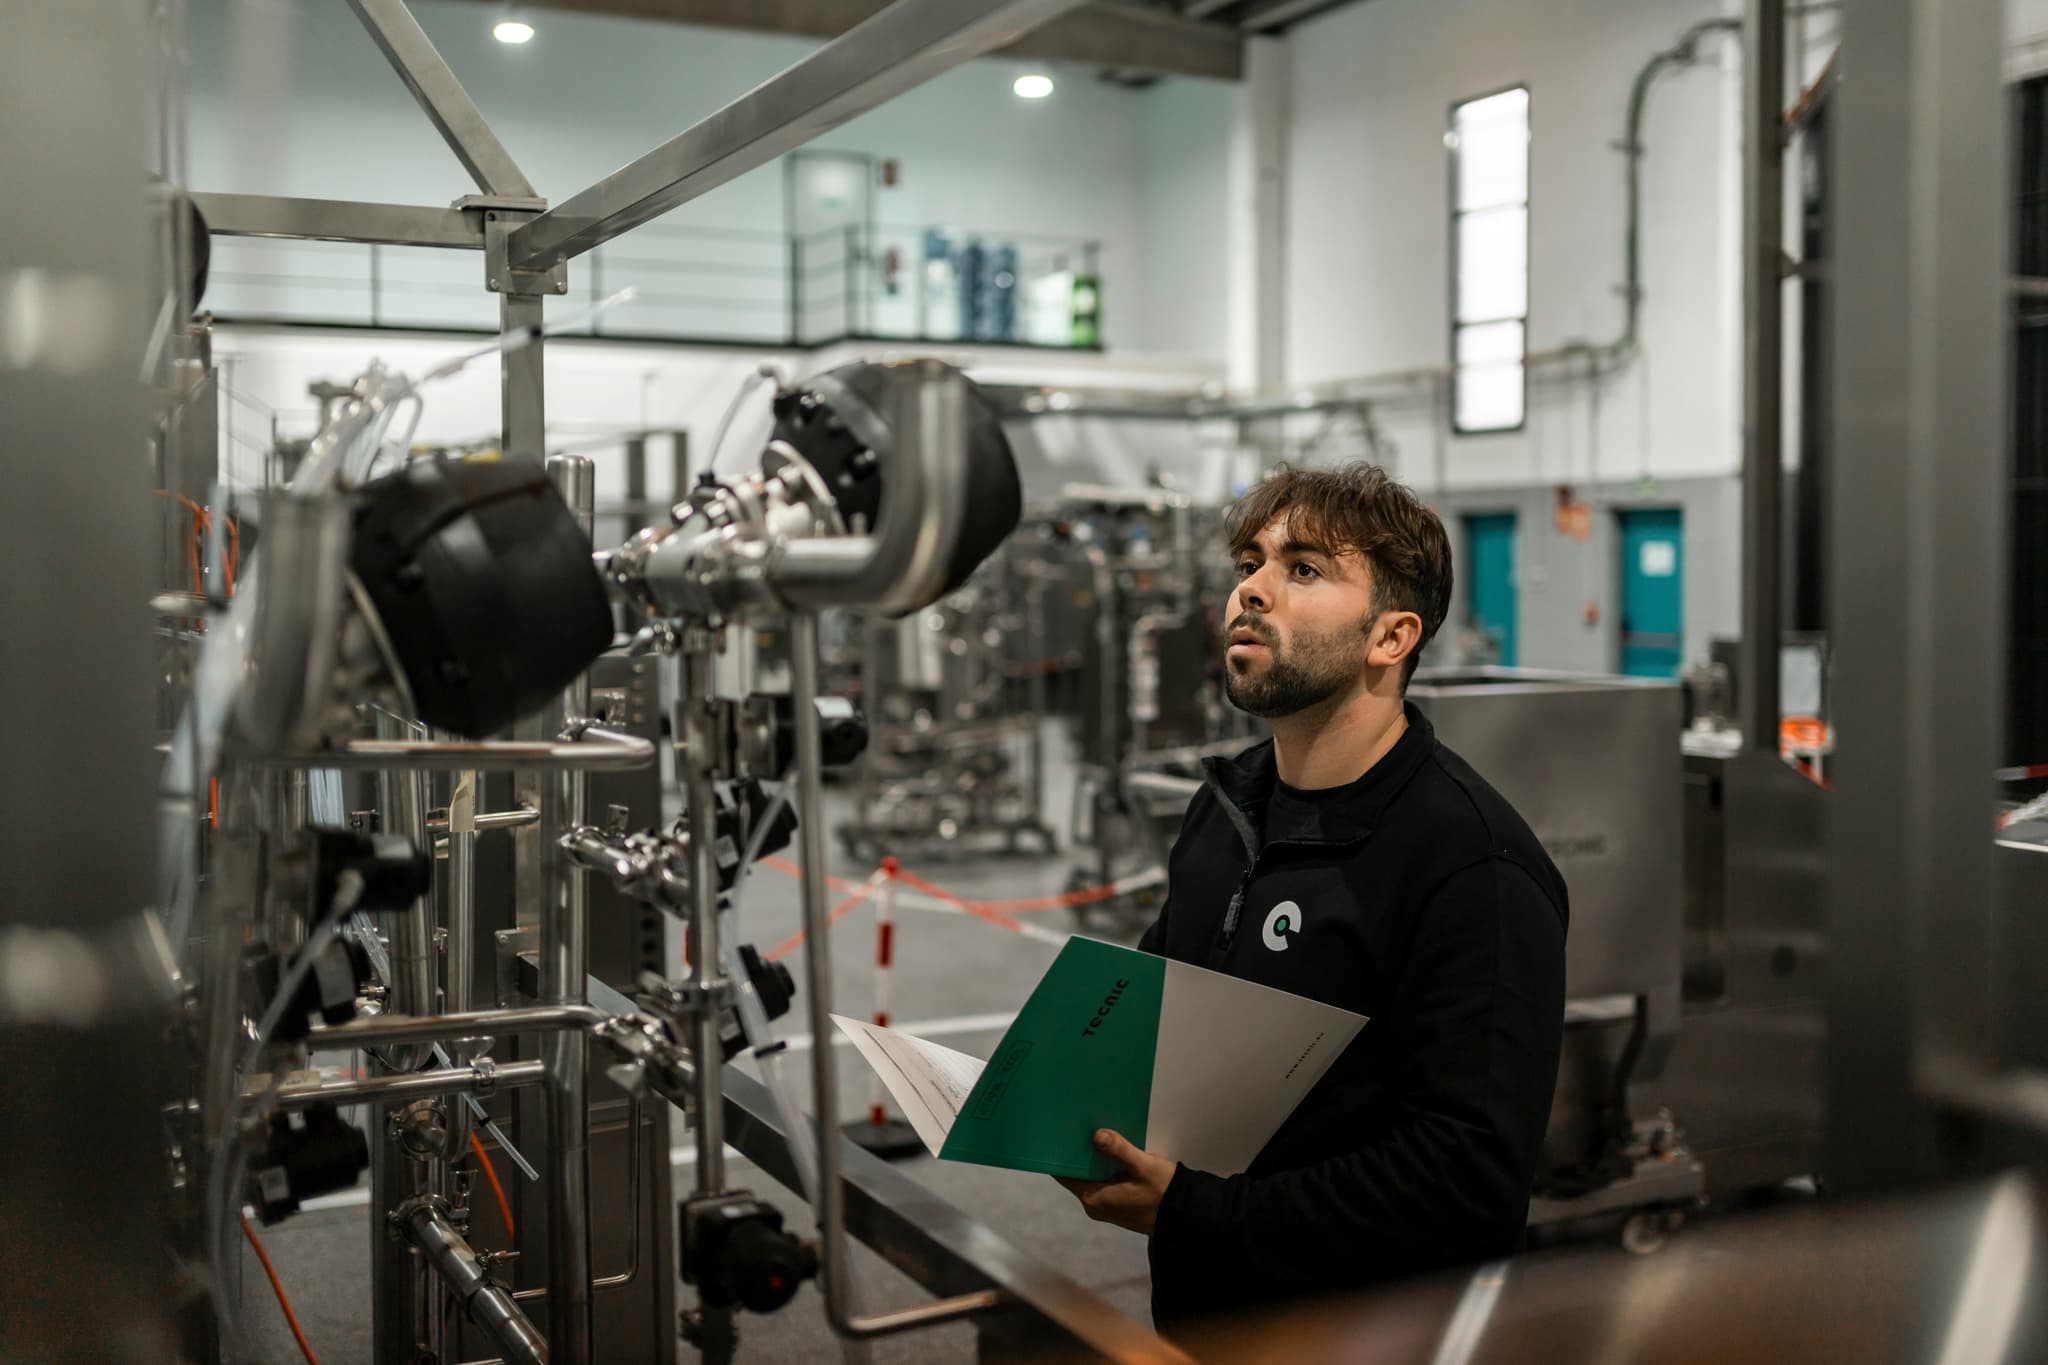
A detailed visual inspection should normally be the starting point for assessing surplus equipment.
Inspectors should look for:
Corrosion and Rust
Surface corrosion can sometimes be cosmetic, but extensive corrosion may indicate deterioration of structural or pressure-containing components.
Particular attention should be given to:
Welded joints
Pressure vessels
Pipe connections
Flanges
Structural frames
Fasteners
Internal surfaces
Areas exposed to moisture or chemicals
Visual testing is an established inspection method for identifying surface defects such as cracks, corrosion and other discontinuities.
Cracks and Structural Damage
Cracks around load-bearing areas, welds, mounting points and structural members can significantly affect equipment reliability.
A simple visual inspection may identify obvious damage, but hidden or difficult-to-detect defects may require additional nondestructive testing.
Leaks
Check for evidence of:
Oil leakage
Hydraulic-fluid leakage
Coolant leakage
Fuel leakage
Process-fluid leakage
Damaged seals and gaskets
Freshly cleaned equipment should also be examined carefully because excessive cleaning or repainting can sometimes make existing leaks or repairs more difficult to identify.
Check Wear on Critical Components
Not all components deteriorate at the same rate.
The condition of critical wear components should therefore be assessed separately.
For mechanical equipment, these may include:
Bearings
Shafts
Gears
Couplings
Seals
Bushings
Belts
Chains
Hydraulic cylinders
Pumps
Valves
Motors
For example, excessive play in bearings, shafts or joints can indicate significant wear even when the external condition of the machine appears acceptable.
The inspection should focus on the components most likely to influence safety, performance and replacement cost.
Review Operating and Maintenance History
A machine's age alone does not determine its condition.
Two identical machines manufactured in the same year can have very different remaining service lives depending on how they were operated and maintained.
Buyers should ask for:
Previous ownership information
Operating hours
Maintenance records
Repair history
Inspection reports
Previous failure records
Replacement-component history
Service intervals
Storage conditions
Operating environment
Heavy-duty or continuous operation can produce significantly different wear compared with intermittent use.
Used-equipment inspection guidance similarly recommends establishing how equipment was previously used and reviewing maintenance records before purchasing.
Verify the Equipment's Operating Hours
Operating hours can be an important indicator of remaining equipment life, particularly for machinery with engines, pumps, compressors and other moving components.
However, hour meters should not automatically be treated as proof of actual usage.
Where possible, compare the recorded hours with:
Maintenance records
Service invoices
Inspection reports
Control-system records
Previous sale documentation
Component replacement dates
A significant inconsistency between these records can justify additional investigation.
Perform Functional Testing
A machine can look excellent and still have serious operational problems.
Functional testing should therefore be performed whenever it is safe and practical.
Depending on the equipment, testing may include:
Starting and stopping
Running under normal load
Checking operating temperature
Measuring pressure
Checking flow rate
Testing controls
Checking vibration
Testing electrical functions
Checking hydraulic movement
Testing emergency systems
Listening for unusual noise
For example, used machinery inspection guidance recommends operating equipment through its normal functions to identify hesitation, excessive play, unusual responses and other operational problems.
A successful test does not guarantee that the equipment is free from defects, but it provides important evidence about its current operating condition.
Use Non-Destructive Testing When Necessary
Visual inspection and functional testing may not be sufficient for high-value or safety-critical equipment.
Non-destructive testing (NDT) allows components to be examined for defects without damaging them. ASNT describes NDT as a group of methods used to evaluate materials, components and structures without harming their usability.
Depending on the equipment and suspected defect, inspection may involve:
Ultrasonic Testing
Ultrasonic testing can be used to detect internal discontinuities and measure material thickness.
It can be particularly useful when evaluating equipment affected by corrosion or potential wall-thickness loss.
Magnetic Particle Testing
Magnetic particle testing can identify surface and near-surface defects in suitable ferromagnetic materials.
Liquid Penetrant Testing
Penetrant testing can reveal surface-breaking defects that may not be visible during an ordinary visual inspection.
Radiographic Testing
Radiography can provide information about internal conditions and is used for applications such as weld and component inspection.
Vibration Analysis
For rotating equipment, vibration analysis can provide valuable information about bearings, imbalance, misalignment, looseness and gear-related problems.
ASNT notes that changes in vibration patterns can reveal developing machinery faults before they result in failure.
Check Electrical and Control Systems
For electrically powered equipment, the mechanical condition is only part of the evaluation.
Inspect:
Motors
Control panels
Wiring
Switchgear
Circuit breakers
Sensors
Drives
PLCs
Displays
Emergency stops
Connectors
Insulation
Grounding
Older equipment may have a good mechanical condition but obsolete electrical or control components.
The availability of replacement parts should therefore be considered before purchase.
Assess Documentation and Traceability
Documentation can significantly affect the value and usability of surplus industrial products.
Important documents may include:
Original manuals
Datasheets
Drawings
Certificates
Inspection reports
Calibration certificates
Maintenance records
Test certificates
Material certificates
Previous repair documentation
Spare-parts lists
For regulated or safety-critical equipment, documentation can be just as important as physical condition.
Inspection organizations emphasize the importance of documenting inspection results and maintaining reliable inspection processes and records.
Determine Whether Parts Are Original or Replaced
Surplus equipment may contain a mixture of original and replacement components.
This is not necessarily a problem. In fact, recently replaced components can increase the value of equipment.
However, buyers should determine:
Which parts were replaced
When they were replaced
Why they were replaced
Whether replacement parts are OEM or aftermarket
Whether modifications were made
Whether modifications were approved
Whether the replacement parts meet the original specifications
Unrecorded modifications can create compatibility, maintenance and safety problems later.
Consider Storage Conditions
Surplus products may have spent months or years in warehouses, outdoor yards or inactive plants.
Storage conditions can significantly influence condition.
Look for evidence of:
Moisture exposure
Dust accumulation
Temperature extremes
UV exposure
Corrosion
Contamination
Improper packaging
Missing protective covers
Degraded seals
Battery deterioration
An unused machine is not necessarily a machine in perfect condition.
Long-term storage can affect lubricants, seals, electrical components, bearings and other parts.
Evaluate Remaining Service Life
The objective of an inspection should not simply be to classify an item as "good" or "bad."
A more useful question is:
How much useful service life remains, and what will it cost to achieve that service life?
For equipment with known degradation mechanisms, engineering assessments can help determine whether continued operation is appropriate.
API 579-1/ASME FFS-1, for example, provides engineering-based fitness-for-service approaches for evaluating damage mechanisms such as corrosion, cracking, fatigue, creep and mechanical overload.
This type of assessment can be particularly important for pressure equipment, piping and other safety-critical industrial assets.
Estimate Repair and Refurbishment Costs
A surplus product should not be evaluated solely on its purchase price.
The actual acquisition cost may include:
Purchase price + inspection + transportation + installation + refurbishment + replacement parts + commissioning
A machine costing less initially may become more expensive than a new or better-maintained alternative if it requires major refurbishment.
Before purchasing, buyers should obtain estimates for critical repairs and replacement components.
Compare Condition With the Intended Application
An item that is acceptable for one application may be unsuitable for another.
For example, equipment previously used in a relatively mild environment may not be appropriate for a process involving:
High temperatures
High pressures
Corrosive chemicals
Abrasive materials
Continuous operation
Hazardous environments
The evaluation should therefore consider the future operating conditions, not just the equipment's current condition.
Use a Condition-Grading System
A standardized grading system can make surplus equipment easier to compare.
For example:
Excellent Condition
Equipment requires little or no refurbishment and is ready for normal operation after standard commissioning.
Good Condition
Equipment shows normal signs of previous use but has no major defects and requires limited maintenance.
Fair Condition
Equipment remains usable but requires repairs, component replacement or refurbishment.
Poor Condition
Equipment has significant wear, damage or missing components and requires substantial investment before operation.
Parts or Salvage Condition
Equipment is not economically suitable for normal operation but may have usable components or materials.
The grading system should always be supported by inspection evidence rather than subjective descriptions alone.
Hire an Independent Inspector for High-Value Equipment
For expensive or safety-critical equipment, an independent inspection can reduce purchasing risk.
An independent inspector or qualified technician can provide an objective assessment of:
Mechanical condition
Structural integrity
Electrical condition
Operational performance
Safety systems
Documentation
Required repairs
Estimated remaining service life
Third-party inspection is particularly useful when the buyer cannot physically inspect the equipment themselves. Used-equipment guidance also recommends consulting an independent inspector or knowledgeable technician when the buyer lacks the expertise to perform the inspection.
Build a Complete Inspection Report
The final inspection should produce a documented record rather than relying on verbal observations.
A useful report should include:
Product identification
Manufacturer and model
Serial number
Inspection date
Inspector details
Photographs
Physical-condition findings
Test results
NDT results, where applicable
Maintenance history
Missing components
Safety concerns
Required repairs
Estimated refurbishment costs
Recommended condition grade
Final purchasing recommendation
Photographs should clearly document defects, corrosion, damaged components and important identification markings.
Make the Purchasing Decision Based on Total Risk
The best surplus industrial purchase is not necessarily the cheapest item.
A better decision considers the relationship between:
Condition + remaining life + performance + documentation + repair cost + safety + availability of parts + purchase price
This approach allows buyers to distinguish between genuinely valuable surplus equipment and products that only appear inexpensive because significant refurbishment costs have been hidden.
For industrial buyers, a structured evaluation process can reduce unexpected failures, improve purchasing decisions and provide greater confidence that surplus equipment will perform as required once installed.
Crude Palm Kernel Oil CAS: 8023-79-8